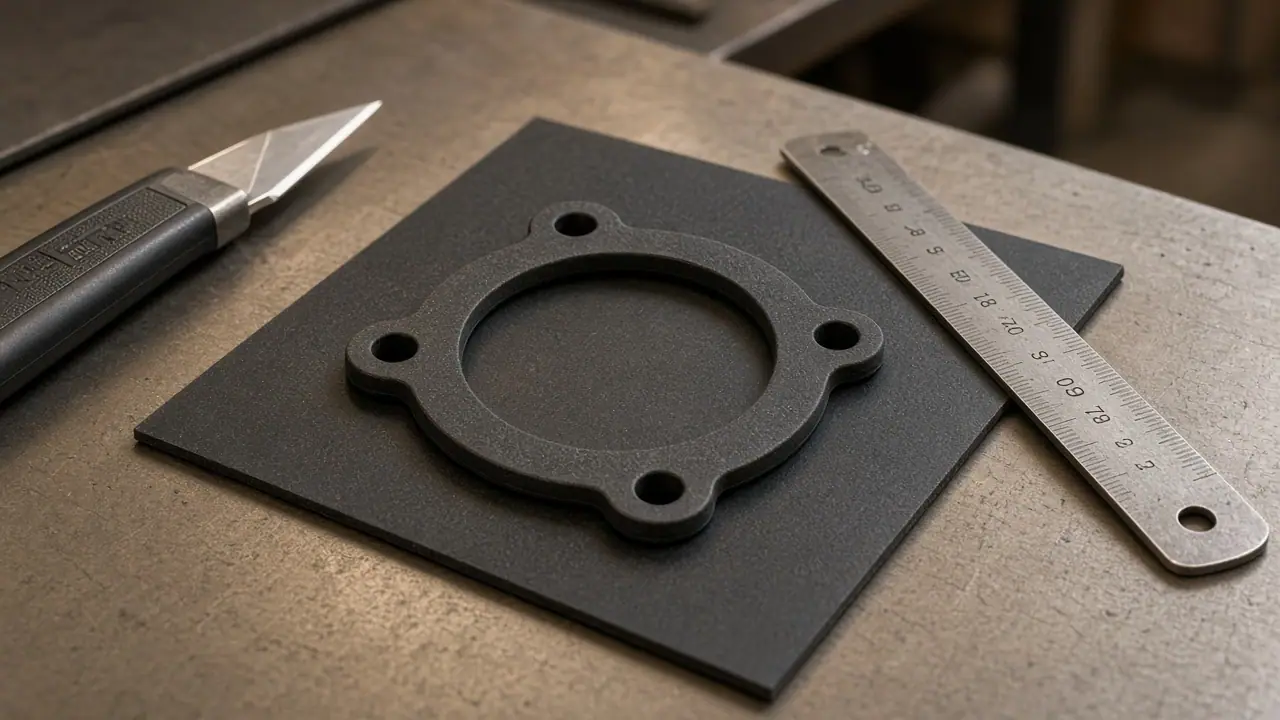
A gasket for one flange, hatch or cover is usually cut from sheet. For a series of identical parts with holes, a mold is more accurate and economical.
A one-off flange, hatch or cover is cut from sheet. We need outer and inner diameter, thickness and medium. EPDM is recommended for water and steam up to +150 °C. NBR for oil up to +120 °C. FKM for hot oil and gas. Take thickness from the flange: a guess either will not compress or will extrude.
The flange surface matters as well. Deep pits, misalignment and an excessive gap cannot be corrected simply with a thicker gasket: check the fit first, then specify compound and compression.
A series of identical gaskets with stud holes is worth molding. Hand-cutting every hole costs more and wanders in tolerance. A mold is usually 10–14 days, then batches are faster.
Fiber gasket sheet and rubber do different jobs. Rubber seals at moderate pressure where spring-back matters. A thin metal flange at high temperature is a separate calculation, not “any 4 mm plate”.
A sample or a photo with a ruler is enough if both diameters and the thickness are visible. Made in Tashkent. +998 90 944 99 40.